Why Is EVA the Ideal Material for Lightweight and Durable Bags?
2026-09-14
1. What Is the Molecular Structure That Makes EVA Both Light and Tough?
EVA is a copolymer of ethylene and vinyl acetate. The vinyl acetate (VA) content typically ranges from 12 to 30 percent. The VA content determines the flexibility, elasticity, and impact resistance of the material. A higher VA content produces a softer, more flexible foam. A lower VA content produces a harder, more rigid material. The closed-cell structure is created during the foaming process. A chemical blowing agent is mixed with the EVA resin and decomposed at a specific temperature, releasing gas that forms millions of tiny bubbles. The cell walls are intact, which means the foam does not absorb water. The density of the foam is controlled by the amount of blowing agent and the molding pressure. In our factory, we produce EVA Bags with foam densities ranging from 0.15 to 0.35 g/cm³, depending on the application requirements.
Why the closed-cell structure matters: An open-cell foam, like a sponge, absorbs water and collapses under repeated compression. A closed-cell foam, like EVA, traps gas in individual cells. The gas provides cushioning, and the intact cell walls provide water resistance. This is why EVA Bags can be submerged in water and still protect the contents inside.
The combination of low density and closed-cell structure gives EVA a specific strength that is higher than most other bag materials. The table below compares the density and mechanical properties of EVA with other common bag materials.
| Material | Density (g/cm³) | Tensile strength (MPa) | Elongation at break (%) | Water resistance |
| EVA foam (closed cell) | 0.15 – 0.35 | 2.5 – 5.0 | 300 – 600 | Excellent (waterproof) |
| PVC (coated fabric) | 1.30 – 1.45 | 15 – 25 | 200 – 350 | Excellent |
| PU (coated fabric) | 1.20 – 1.35 | 12 – 20 | 250 – 400 | Good (not fully waterproof) |
| Nylon 6,6 (fabric) | 1.14 | 70 – 85 | 20 – 40 | Poor (absorbs water) |
| TPU (coated fabric) | 1.20 – 1.25 | 25 – 40 | 400 – 600 | Excellent |
The density of EVA is 4 to 8 times lower than that of PVC or PU. This means that a bag made from EVA foam will weigh significantly less than a bag made from a coated fabric. The tensile strength of EVA is lower than that of PVC or nylon, but the closed-cell structure provides impact absorption that these materials cannot match. The elongation at break is high, which means the material can stretch without tearing.
2. How Does EVA Compare to Other Materials in Real-World Bag Applications?
The performance of a bag material is not determined by a single property. It is determined by the combination of properties that matter for the specific application. The table below compares EVA with other materials across five criteria that are important for bag design.
| Criteria | EVA | PVC | PU | Nylon |
| Weight (for a 1L capacity bag) | 80 – 120 g | 250 – 350 g | 200 – 300 g | 150 – 220 g |
| Water resistance | Waterproof | Waterproof | Water resistant | Absorbs water |
| UV resistance | Excellent | Poor (yellowing) | Moderate | Moderate |
| Cold flexibility (-20°C) | Excellent | Poor (brittle) | Moderate | Moderate |
| Cost per kg (raw material) | $1.80 – $2.50 | $1.20 – $1.60 | $2.50 – $3.50 | $3.00 – $4.00 |
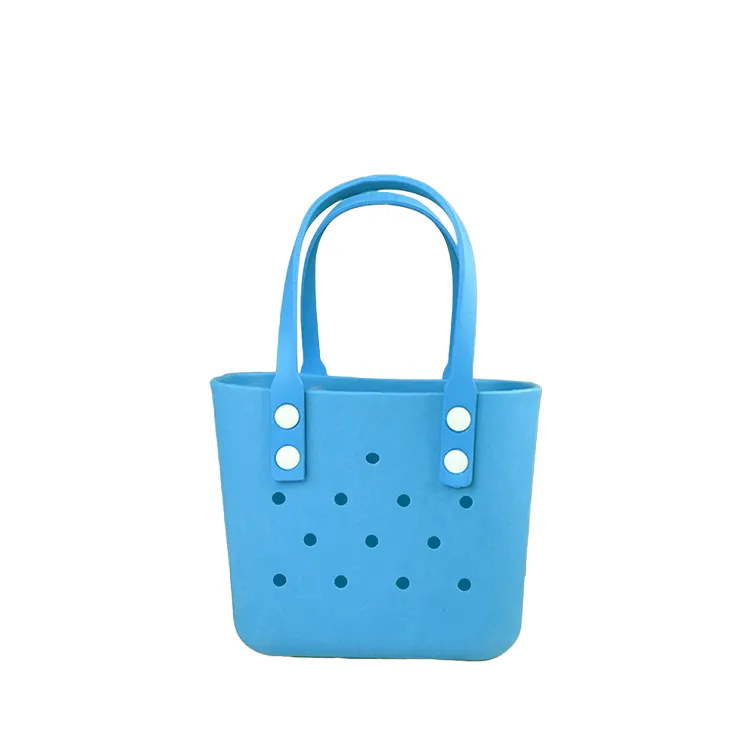
The weight advantage of EVA is the most visible benefit. A 1L EVA Bags weighs 80 to 120 grams, compared to 250 to 350 grams for a PVC bag of the same capacity. For a consumer product, this weight difference is immediately noticeable. The UV resistance of EVA is also superior to PVC. PVC yellows and becomes brittle when exposed to sunlight. EVA retains its color and flexibility after years of outdoor use. The cold flexibility of EVA is another advantage. PVC becomes brittle at -10°C, while EVA remains flexible at -20°C or lower.
Application example: A tool bag made from EVA foam (density 0.25 g/cm³) and a tool bag made from PVC-coated polyester were tested side by side. The EVA bag weighed 340 grams. The PVC bag weighed 920 grams. After 6 months of daily use in a maintenance workshop, the EVA bag showed no cracking or delamination. The PVC bag showed cracks at the seams and the coating had begun to peel.
3. What Processing Parameters Determine the Quality of EVA Bags?
The quality of an EVA Bags depends on the molding process. EVA foam is typically produced by compression molding or injection molding. In compression molding, the EVA resin, blowing agent, and crosslinking agent are mixed and placed in a mold. The mold is heated under pressure. The blowing agent decomposes, and the crosslinking agent creates chemical bonds between the polymer chains. The crosslinking is what gives EVA its resilience and dimensional stability. The table below shows the key processing parameters for our EVA Bags.
| Process parameter | Typical value | Effect on EVA Bags quality |
| Molding temperature | 160 – 180°C | Controls blowing agent decomposition and crosslinking rate |
| Molding pressure | 5 – 15 MPa | Controls density and cell structure |
| Crosslinking agent | Dicumyl peroxide (DCP), 0.5 – 1.5 phr | Determines resilience and compression set |
| Blowing agent | Azodicarbonamide (ADC), 2 – 5 phr | Determines density and cell size |
| Molding time | 10 – 25 minutes | Ensures complete crosslinking and foaming |
| Cooling rate | Controlled, 2 – 5°C/min | Prevents warping and shrinkage |
Our factory uses a fully automated compression molding line for EVA Bags. The temperature, pressure, and time are controlled by a PLC system. Every batch is tested for density, hardness, tensile strength, and compression set. We also perform a water absorption test to verify that the closed-cell structure is intact.
4. How Do You Verify the Durability of EVA Bags Before Mass Production?
Before committing to mass production, it is essential to verify that the EVA Bags will meet the durability requirements of the intended application. There are four standard tests that we perform in our factory. The first is the abrasion test, which measures the resistance of the surface to rubbing. The second is the flex fatigue test, which measures the resistance to repeated folding. The third is the impact test, which measures the ability to absorb shock without cracking. The fourth is the UV aging test, which measures the color and property retention after exposure to simulated sunlight. The table below shows the test methods and the acceptance criteria for a typical EVA Bags application.
| Test | Method | Acceptance criteria |
| Abrasion resistance | Taber abrasion, 500 g load, 1000 cycles | Weight loss < 0.1 g |
| Flex fatigue | ASTM D430, 100,000 cycles | No cracking or delamination |
| Impact resistance | Drop test, 1 kg weight from 1 m | No fracture or permanent deformation |
| UV aging | QUV, 500 hours | Color change ΔE < 3, no surface tackiness |
Jinjiang Zhuoling New Materials Technology Co., Ltd. provides a full test report with every batch of EVA Bags. We also offer pre-production samples for customer evaluation. Our engineering team can assist with material selection and mold design to ensure that the final product meets your performance requirements.
Frequently Asked Questions About EVA Bags and Material Selection
Summary for Product Developers and Sourcing Managers
EVA is the ideal material for lightweight and durable bags because it combines low density with high resilience, waterproof performance, UV resistance, and cold flexibility. The closed-cell structure provides impact absorption that coated fabrics cannot match, and the weight is 4 to 8 times lower than PVC or PU. The processing parameters, particularly the VA content, density, and crosslinking, determine the final performance of the EVA Bags. When selecting a supplier, verify the material specifications and request test reports for abrasion, flex fatigue, impact, and UV aging. Jinjiang Zhuoling New Materials Technology Co., Ltd. has been manufacturing EVA Bags for over 12 years and supplies to brands and distributors worldwide.
Jinjiang Zhuoling New Materials Technology Co., Ltd. manufactures EVA Bags in a range of densities, colors, and shapes. We provide full material test reports and pre-production samples for evaluation. Our engineering team can assist with material selection and mold design.